Introduction:
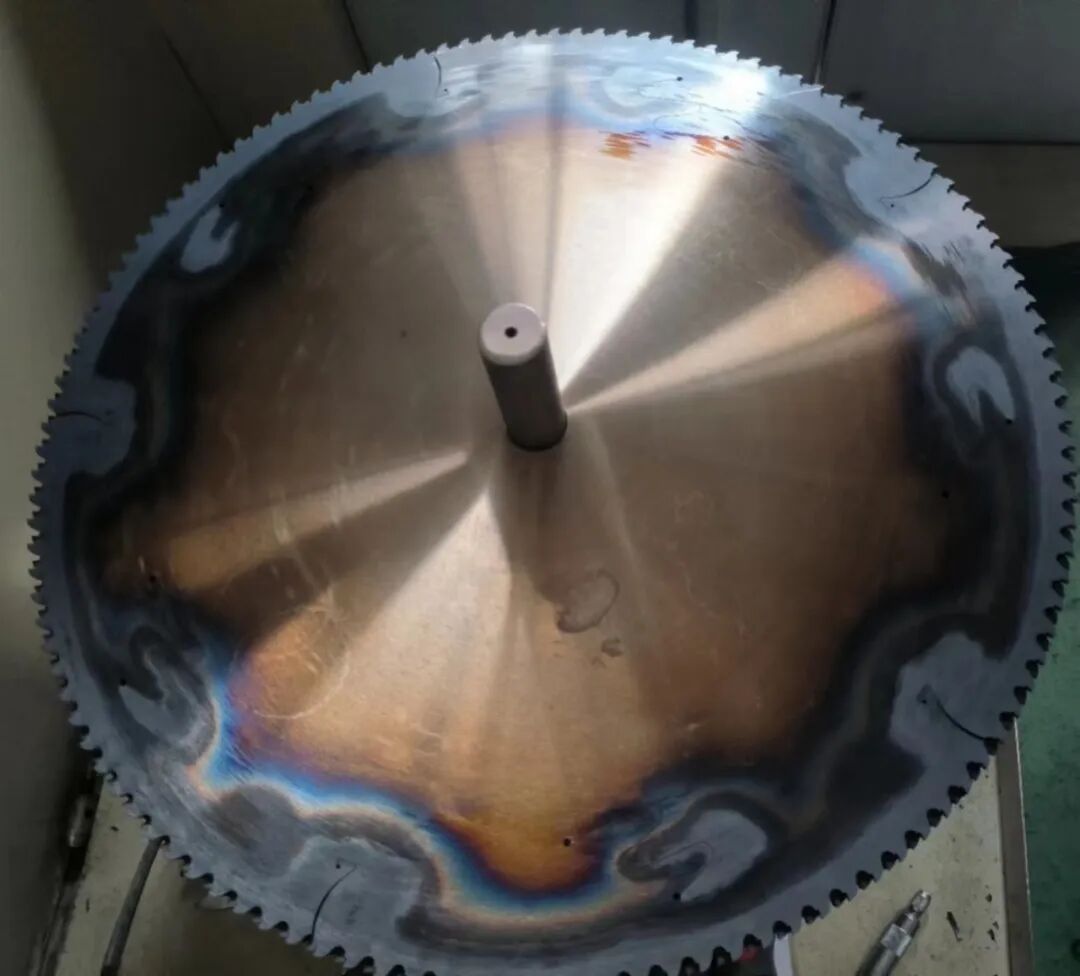
As industrial production becomes increasingly automated, operators need to manage more machines. This raises customers’ requirements for grinding wheel service life. To meet this demand, our company has invested R&D resources to develop a longer-life CBN grinding wheel for machining alloy saw blade substrates. It is suitable for workpieces made of 65Mn, SKS51 and 75Cr1.
Customer Challenge:
The customer stated that their existing grinding wheels delivered acceptable service life, but they were looking for a longer-lasting option to better fit their production. To address this, we conducted on-site tests with our new wheel at the customer’s facility.
Equipment & Grinding Wheel:
Grinding Wheel Specification: 350×127×10×30×40T
Customer’s Machine: Automatic Surface Grinder
Grinding Wheel Dressing Procedure:
After mounting the new wheel, runout must be eliminated. The dressing steps are as follows: Fix a #46 white alumina wheel onto the rotary table. Set rotary table speed: 400 rpm Grinding wheel speed: 100 rpm Feed rate: 1500 mm/min Infeed per pass: 0.02 mm on each side Approximately 200 passes are required for full dressing. You can verify dressing quality by sound: a continuous, steady sound indicates proper dressing.
Tip: An out-of-round wheel will generate chatter marks on the saw blade substrate and compromise geometric tolerances.
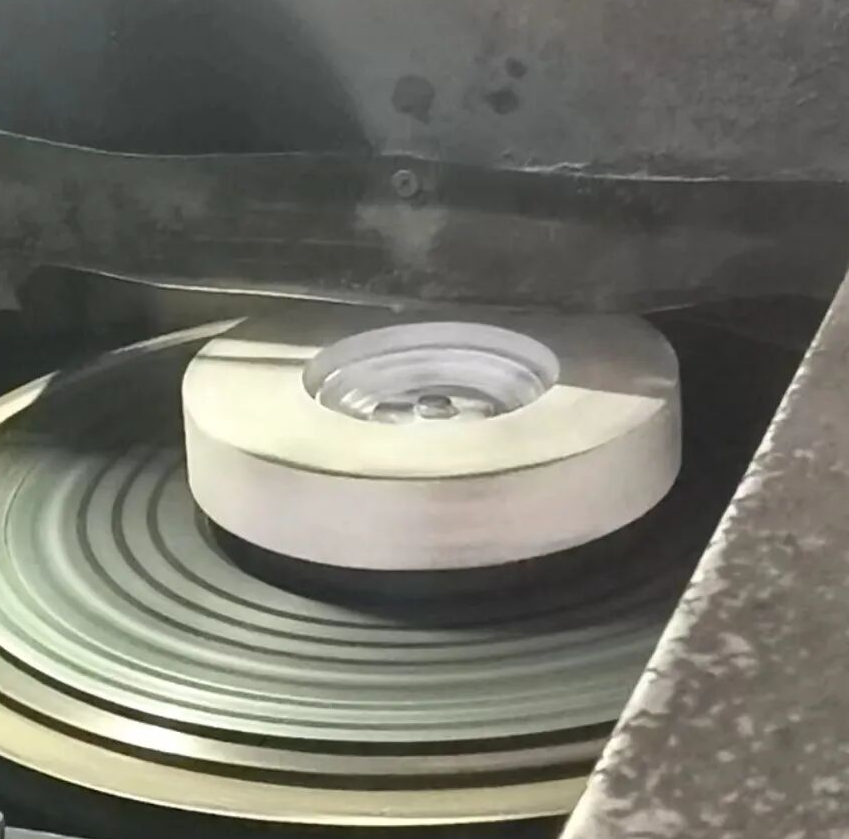
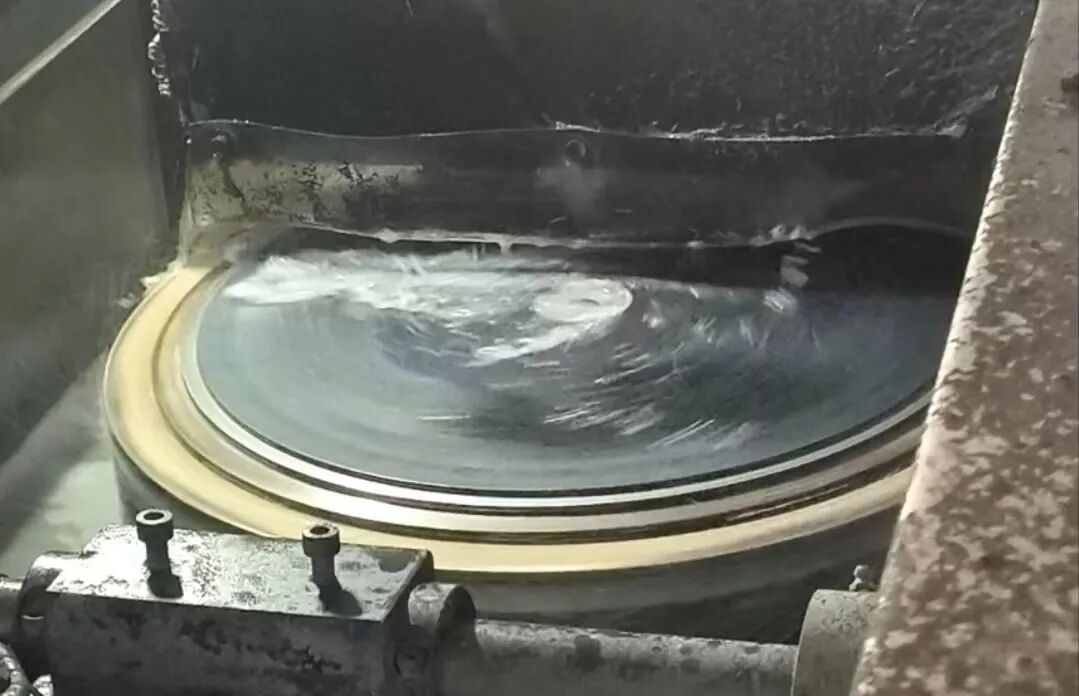
Grinding Parameters:
Workpiece: Saw blade substrate, Diameter 400 mm
Cutting speed: 45 m/s
Feed rate (Rough / Finish grinding): 2500 / 1000 mm/min
Rotary table speed: 600 rpm
Infeed (compensation): 0.002 mm per 2 pieces
Blank thickness: 3.4 mm
Finished thickness: 3.2 mm
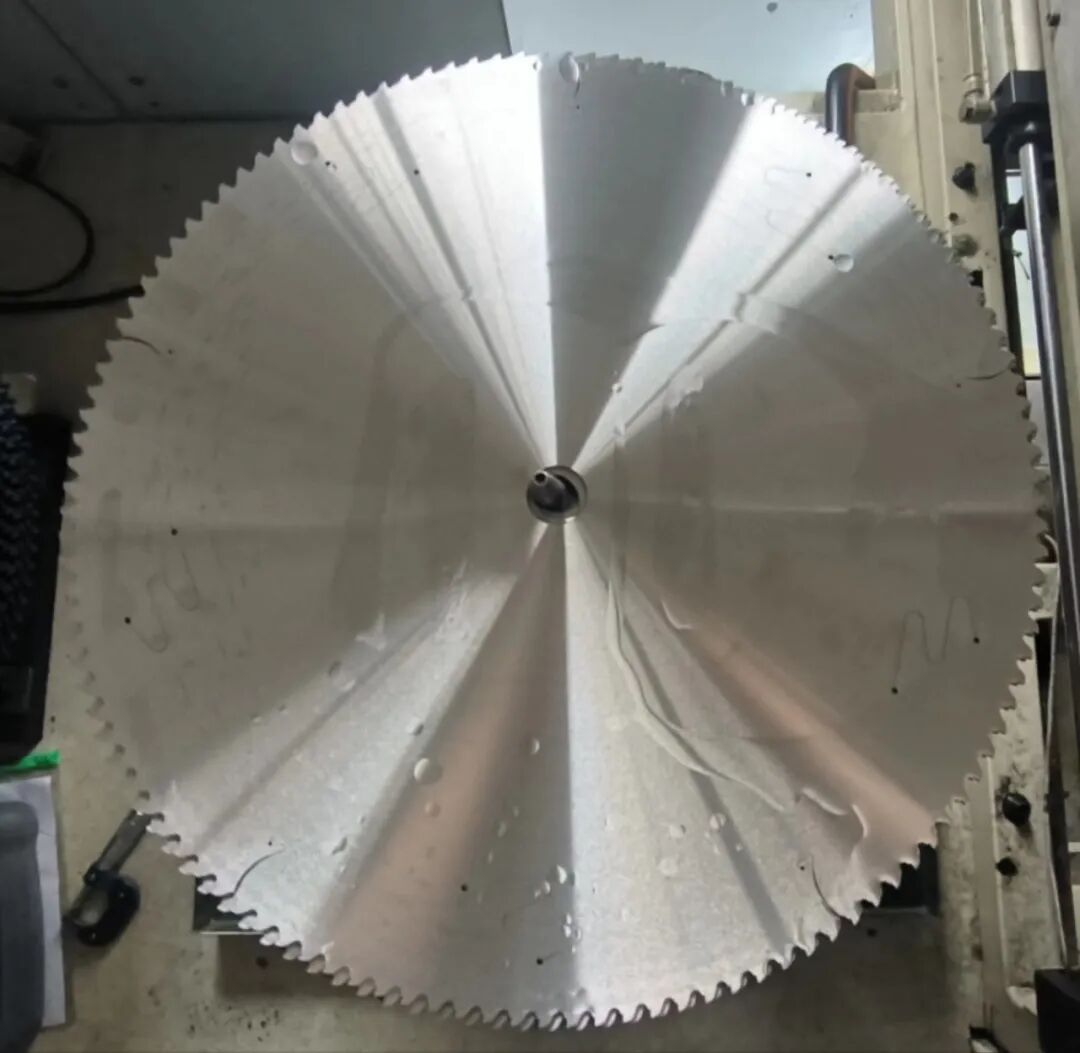
Dressing Result:
Before Dressing | After Dressing
Wheel Wear Compensation:
Setting: 0.002 mm compensation for every 2 saw blades